Opening problem frame
Factories will soon expect batteries to behave like predictable machinery, but today they don’t—and that mismatch breaks production lines. A single misrouted rack, a misread state-of-charge, or a thermal event can halt an entire assembly cell. That’s why an energy storage cabinet sitting on a mezzanine isn’t just hardware; it’s a potential single point of failure unless service partners provide clear, factory-grade protocols from delivery to decommissioning.
What actually fails and why
Problems recur in patterns. Spot the pattern and you fix more than a symptom.- Mechanical fit issues: cabinets that don’t match planned footprints or access routes.- Integration blind spots: BMS communications that never map to the plant’s SCADA.- Safety mismatches: containment and ventilation designed for prototypes, not production volumes.- Lifecycle gaps: no plan for cell replacement, firmware updates, or end-of-life recycling.Each is a discrete engineering problem. Each has cost, downtime, and compliance consequences.
Factory integration realities — a grounded case
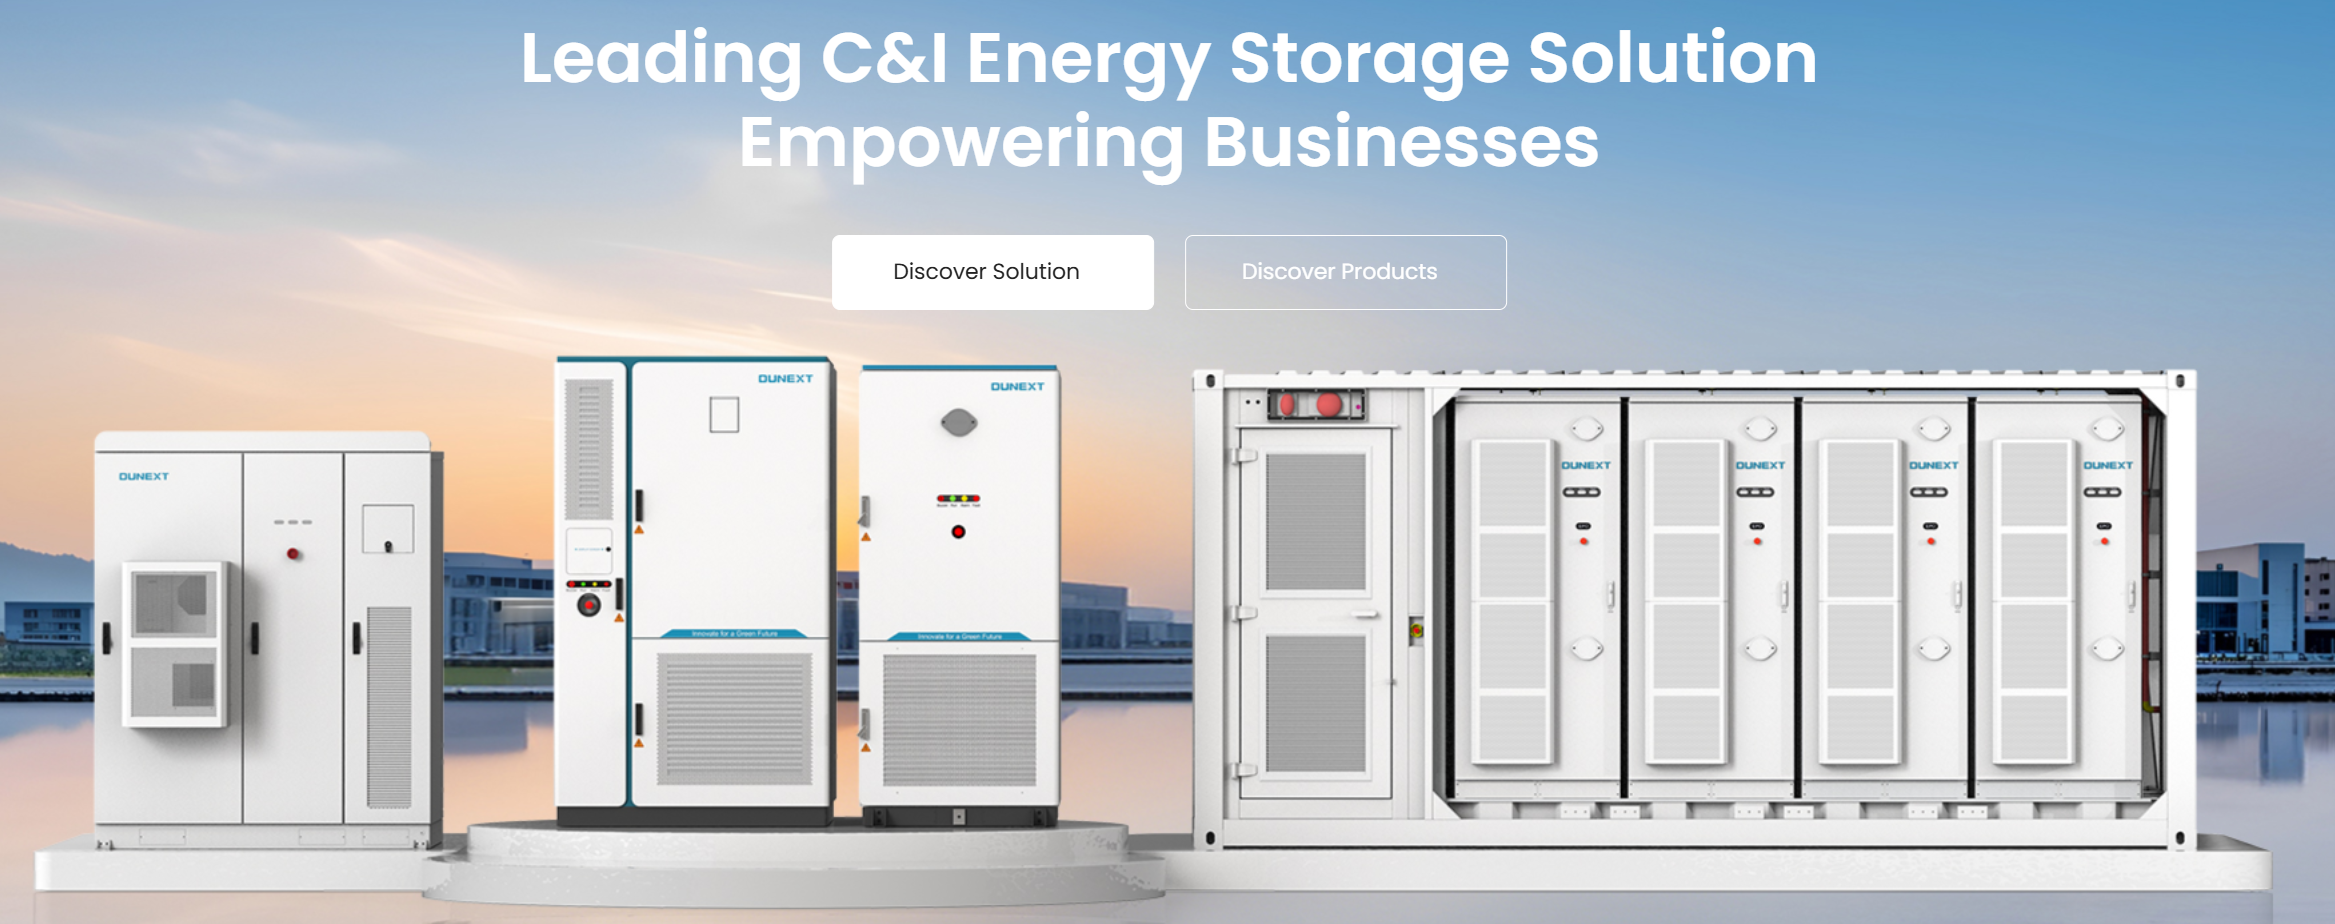
Imagine a southern China production corridor where rows of BESS units arrive for line-by-line integration—workflows tighten or stall depending on how well the storage hardware was specified. That Shenzhen manufacturing cluster taught integrators a hard lesson: standardized dimensions and a documented mechanical envelope save days on the dock. For factory-scale installations you also need documented use-cases for battery energy storage cabinet factory b2b applications so teams can pre-map communication channels, spare parts lists, and safety zones before trucks roll in.
Technical guardrails you should demand
Insist on measurable checkpoints rather than vague promises.- Mechanical: delivered cabinets must match CAD models within stated tolerances.- Electrical: commissioning tests should include interlock validation, charge/discharge acceptance, and harmonic analysis.- Safety: thermal propagation tests and validated containment plans—refer to recognized test frameworks such as UL 9540A for thermal response and IEC series guidance for cell-level safety.- Documentation: complete firmware baselines, BOMs, and firmware rollback procedures.These guardrails come from hands-on projects and test labs; treat them as non-negotiable.
Operational playbook — concrete steps
Follow a short, repeatable flow.1. Receive: Verify mechanical envelope and tagging against CAD before offloading. 2. Inspect: Run dry-power tests and communication handshakes on the dock. 3. Commission: Execute automated scripts that validate BMS, relays, and DERMS links. 4. Harden: Install physical shields, fire suppression points, and clear maintenance pathways. 5. Maintain: Schedule firmware audits and cell health sampling at fixed intervals.Common mistakes: skipping dock-level testing, ignoring cable bend radii, and assuming firmware compatibility. Fix those and you cut integration days into hours.
Choosing partners and equipment
Pick partners who show test logs, not glossy specs. Ask for field reports from peers who run continuous production lines. Confirm the vendor supplies:- spares kits matched to the installed fleet,- repeatable commissioning scripts,- training modules for on-site technicians.Equipment selection matters, but protocol adherence matters more. Hardware without a service protocol is an expensive prototype.
Final synthesis
This is a pragmatic future: factories will treat BESS like essential plant equipment, and service partners who codify delivery, commissioning, and lifecycle operations will be the ones factories trust. The path forward demands discipline—detailed envelopes, testable interfaces, and repeatable maintenance cycles—so the storage hardware becomes part of the plant’s predictable rhythm, not an intermittent risk. In that working future, partners such as Dunext supply both the cabinets and the procedural clarity factories need to keep lines moving.